Featured Articles

Boost Your Website Traffic with High Quality DA/PA 40+ Backlinks
Apr 7, 2023

In today’s competitive world, one must be knowledgeable about the latest online bus...
Oct 12, 2018
With the rapid development of the petrochemical industry, stainless steel materials(such as stainless seamless steel pipe) have been widely used, which has also put forward higher requirements for the welding of pipes and plates, and has gradually eliminated the previous stainless steel arc welding priming method. When using argon arc welding for primer welding, argon arc welding for primer is faster and cleaner than arc welding. At the same time, some problems also arise.
During the welding process, since the back of the stainless steel argon arc welding primer is easily oxidized and causes defects, back protection measures must be taken to ensure the mechanical properties and corrosion resistance of the weld. Therefore, effective protection must be taken when welding stainless steel tubes.
1. Protective cover filled with argon protection method
This method is often used in the welding of large-diameter stainless steel pipes. The protective cover is connected to a metal pipe and an argon gas hose. The argon gas valve is opened to fill the protective cover with argon gas. The advantages of this method are concentrated protection and less argon gas waste.
2. Local argon filling protection method
For pipelines with small local space and short dimensions, it is easy to use local protection. Method: seal the pipeline welding joint with tape (to prevent air leakage), seal both ends of the pipeline with sponge, rubber, paper shell, etc., and connect the argon hose from Insert one end and fill it with argon gas, and it is best to make a small hole in the sealing area of the other end of the pipe. This will facilitate the final welding joint and will not cause dents due to excessive internal pressure;
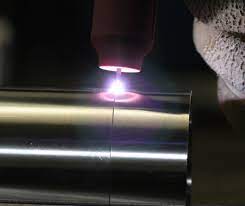
During welding, in order to prevent a large amount of argon gas from being discharged from the weld seam, the weld sealing tape should be torn off and welded in sections. This can reduce the loss of argon gas and effectively protect the weld seam. This method is characterized by waste, slow argon filling, and high cost.
3. Direct argon filling method in the welding joint
For pipelines that are too long and have slightly larger diameters, local argon filling is too wasteful, the quality cannot be guaranteed, and the project cost is too high. In order to save costs, the direct argon filling method at the welded joint can be used.
4. Plugging method on both sides of the weld seam
Process the sponge into a plug with a slightly larger diameter for the pipe and connect the two pieces of sponge with a wire at a distance of 300-400 mm to make a double plug. Connect one end of the plug to a longer section of steel wire. When the two pieces meet, plug the plug at the key point first. Weld 150-200 mm on both sides of the weld. The long iron wire at one end should be longer than the length of the pipe at one end of the weld and expose the pipe end. One end of the small metal pipe is flattened, and the other end is connected to the argon hose. The flattened end is inserted into the aligned weld. Seam, fill with argon, and the best insertion direction is the uppermost part, so that before the bottom welding of the final joint, the small tube can be pulled out and welded by the remaining gas in the pipe. After welding, use wire to pull out the plug.
5. Argon gas protection judgment
The protective effect of argon gas can be judged according to the color of the internal weld, so that the operator can adjust the argon gas according to the color to achieve the best protection effect. White and golden yellow are most suitable.
Article source: https://article-realm.com/article/Business/54467-Back-protection-method-for-welding-stainless-steel-tube.html
Comments
Reviews
Most Recent Articles
- Oct 3, 2026 What Is a Crypto Exchange Clone Script and How Does It Work? by Benjamin Valor
- Oct 2, 2026 Business Stories Explaining Changes Across the Modern Market by backily
- Oct 1, 2026 Humidity Sensor Market: Applications in Greenhouses and Precision Agriculture by Dipak Straits
- Oct 1, 2026 Home Shopping Market: The Rise of Direct-to-Consumer Retail Models by Dipak Straits
- Oct 1, 2026 Global Medical Aesthetics Market: Innovations in Facial Rejuvenation by Dipak Straits
Most Viewed Articles
- 10652 hits Market Overview: Membrane Contactor Industry 2025 by Terra Logistics
- 8575 hits Mist Sprayer Pumps Market Demands, Trends, Industry Analysis, Segmentation by 2032 by ellamrfr
- 6774 hits Next-Gen Connectivity and the Rising Demand for RF Semiconductors by James Cameroon
- 5685 hits Digital Printing Packaging Market by Technology, Application, and Region by James Cameroon
- 4715 hits Flexographic Printing Plates Market Size, Share, Report 2024-32 by ellyse perry
Popular Articles
In today’s competitive world, one must be knowledgeable about the latest online business that works effectively through seo services....
81500 Views
Walmart is being sued by a customer alleging racial discrimination. The customer who has filed a lawsuit against the retailer claims that it...
62287 Views
Are you caught in between seo companies introduced by a friend, researched by you, or advertised by a particular site? If that is...
37314 Views
Facebook, the best and most used social app in the world, has all the social features you need. However, one feature is missing. You cannot chat...
23582 Views
If you have an idea for a new product, you can start by performing a patent search. This will help you decide whether your idea could become the...
14847 Views

Moving becomes easy when you have the right moving accessories. These moving accessories help secure and protect your item by ensuring that no harm...
13227 Views

A lot of us look forward to the result of moving and not the process itself. It is pretty typical behavior, though. As modern people, many things...
13150 Views

Building a custom home is an exciting adventure. It’s your chance to bring your vision to life and create an area that sincerely displays...
12911 Views

Moving from one state, city, or even to a whole different county, is something that is either dictated by choice or circumstance. This is because,...
11972 Views

A membrane contactor is a device that enables the transfer of components between two immiscible phases, typically a gas and a liquid, through a...
10652 Views
Statistics
| Members | |
|---|---|
| Members: | 17144 |
| Publishing | |
|---|---|
| Articles: | 79,592 |
| Categories: | 202 |
| Online | |
|---|---|
| Active Users: | 1532 |
| Members: | 0 |
| Guests: | 1532 |
| Bots: | 9615 |
| Visits last 24h (live): | 7735 |
| Visits last 24h (bots): | 64433 |


