Featured Articles

In today’s competitive world, one must be knowledgeable about the latest online bus...
Oct 12, 2018
High-frequency straight seam welded pipe (ERW welded pipe) sizing means that the welded pipe is rolled through specific passes of roller butt welding, and the round pipe or special-shaped pipe with irregular size and shape is adjusted into a finished pipe. Regular shapes and sizes that meet standard requirements. There are four basic functions of diameter technology.
1. Determine the basic size and shape of the welded pipe
(1) Circle→Circle, by adjusting the sizing round roller, the irregular round tube sized after the extrusion roller is adjusted into a finished round tube with qualified cross-sectional shape and size. Measuring the roundness of a pipe depends not only on the distribution of the actual tolerance zone, but also on the ovality of the pipe. The ovality is generally 80% of the limit deviation. In practice, although some welded pipes do not exceed the tolerance, they exceed the ovality tolerance or tolerance zone and are close to the limit value. , this also needs to be adjusted.
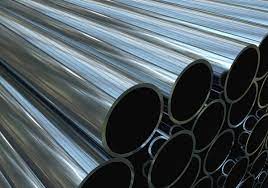
(2) Circle → Square, from round tube to special-shaped tube. By adjusting the special-shaped rolling roller, the circular cross-section welded pipe after the extrusion roller is adjusted into special-shaped pipes with different cross-sectional shapes and sizes. In fact, no matter how complex the special-shaped pipe is, its adjustment process revolves around surface, angle, and shape tolerances.
(3) Square → Square. In the direct forming process, for special-shaped tubes whose size and shape do not meet the standard requirements after extrusion rollers, the shape and size tolerances can be met by adjusting the special-shaped rollers.
2. Reduce stress
After the welded pipe is formed, welded and cooled, it becomes a fixed diameter welded pipe. In this pipe body, a large amount of longitudinal residual stress and transverse residual stress are accumulated. If it is not shaped and rolled by the sizing roller, part of the residual stress in the pipe will be reduced. Only the bending caused by stress will prevent the normal production of welded pipes, and the bent welded pipe itself indicates the tendency of longitudinal residual stress in the pipe.
Due to the reduction mechanism of longitudinal residual stress, sizing welded pipes always rise along the weld seam. When the upturned welded pipe is rolled by several flat and vertical sizing rollers arranged in a straight line, the welded pipe obtains upward rolling force and the welded pipe becomes upturned. The weld seam changes from a concave arc to a straight line and then elongates, which increases the tensile stress of the weld seam and reduces the compressive stress of the weld seam, thereby reducing the vector algebraic sum of the residual stress of the weld seam and reaching a basic balance. The concave arc on the back side of the weld is also rolled straight, which increases the compressive stress on the back side of the weld and reduces the residual tensile stress in this part. During this increase and decrease process, the longitudinal residual stress of the welded pipe tends to be basically balanced. In this way, the longitudinal residual stress represented by the weld position and the back side of the weld is very small. The welded pipe after leaving the sizing roller is straight, and the same is true for left and right bends.
3. Achieve basic straightness
In the practice of welded pipe production, there are two understandings of straightness. First, the straightness specified by the international regulations is not more than 2‰ for round pipes and 3‰ for special-shaped pipes. Another is the straightness used. Indicator requirements are determined by both parties. It is agreed that the former is suitable for "market goods" and users are not fixed, while the latter is suitable for specific users with requirements. Regardless of the straightness, only the rolling of the sizing roller can balance the internal stress of the pipe and achieve the basic straightness of the welded pipe.
4. Improve the surface quality of welded pipes
Make the weld smooth. The surface of the weld after removing the outer burrs is always connected to the outer circle of the welded pipe instead of a tangent. There are edges and corners during the connection. You can always feel the weld on the surface of the angular pipe when you touch it with your hand. It's not beautiful. After rolling with several sizing rollers, the edges and corners of the weld surface and pipe surface can be removed to achieve smoothness.
Reduces surface dents and scratches. From pipe forming to welding, rolling and high temperature welding 20 to 30 rolls (more rolling will be done) and high temperature welding. No matter which link it is, it may leave scars on the surface of the welded pipe. However, after the sizing roller is rolled, some scars and marks will fade and have no hand feel. In order to prevent the sizing section itself from being scratched, it is necessary to carefully adjust the symmetry of the sizing passes, apply the rolling force correctly, and ensure that there are no surface defects such as indentations and scratches on the surface of the welded pipe.
Tip: If ERW (resistance welded) pipe is ASTM A53 Grade B, the weld should be heat treated at a minimum of 1000°F [540°C]. Untempered martensite is retained in this manner.
If ASTM A53 B erw cold expansion pipe, then the expansion should not exceed 1.5% of the required outside diameter.
Article source: https://article-realm.com/article/Business/61627-Basic-process-of-ERW-pipe-sizing.html
Comments
Reviews
Most Recent Articles
- Oct 24, 2026 StaticStop to Exhibit at SMTA Space Coast Expo and Tech Forum by Dinesh Kumar
- Oct 24, 2026 Study Business Analytics in Vietnam: Scope, Top Universities, Fees & Career Prospects by Mahesh Mysto
- Oct 23, 2026 AI-Powered Healthcare Imaging in 2026: How Computer Vision Is Transforming Medical Diagnostics by HyprForge
- Oct 23, 2026 What Factors Affect the Service Life of 304 Stainless Steel Pipes? by Jane Tian
- Oct 23, 2026 Acceptance criteria for 304 stainless steel pipe by Jane Tian
Most Viewed Articles
- 10686 hits Market Overview: Membrane Contactor Industry 2025 by Terra Logistics
- 8597 hits Mist Sprayer Pumps Market Demands, Trends, Industry Analysis, Segmentation by 2032 by ellamrfr
- 6801 hits Next-Gen Connectivity and the Rising Demand for RF Semiconductors by James Cameroon
- 5706 hits Digital Printing Packaging Market by Technology, Application, and Region by James Cameroon
- 4741 hits Flexographic Printing Plates Market Size, Share, Report 2024-32 by ellyse perry
Popular Articles
In today’s competitive world, one must be knowledgeable about the latest online business that works effectively through seo services....
81605 Views
Walmart is being sued by a customer alleging racial discrimination. The customer who has filed a lawsuit against the retailer claims that it...
64070 Views
Are you caught in between seo companies introduced by a friend, researched by you, or advertised by a particular site? If that is...
37364 Views
Facebook, the best and most used social app in the world, has all the social features you need. However, one feature is missing. You cannot chat...
23644 Views
If you have an idea for a new product, you can start by performing a patent search. This will help you decide whether your idea could become the...
14899 Views

Moving becomes easy when you have the right moving accessories. These moving accessories help secure and protect your item by ensuring that no harm...
13270 Views

A lot of us look forward to the result of moving and not the process itself. It is pretty typical behavior, though. As modern people, many things...
13224 Views

Building a custom home is an exciting adventure. It’s your chance to bring your vision to life and create an area that sincerely displays...
12964 Views

Moving from one state, city, or even to a whole different county, is something that is either dictated by choice or circumstance. This is because,...
12087 Views

The report is titled as ‘Recombinant Cell Culture Supplements Market: Opportunity Analysis and Future Assessment 2022-2030’. An...
11870 Views
Statistics
| Members | |
|---|---|
| Members: | 17226 |
| Publishing | |
|---|---|
| Articles: | 79,838 |
| Categories: | 202 |
| Online | |
|---|---|
| Active Users: | 1155 |
| Members: | 1 |
| Guests: | 1154 |
| Bots: | 11911 |
| Visits last 24h (live): | 5908 |
| Visits last 24h (bots): | 47247 |


